Plastic Chain Plate Conveyor for Food and Beverage Production

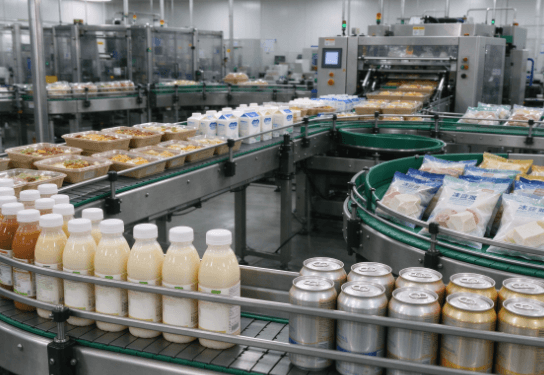
A plastic chain plate conveyor for food is a modular conveying system designed to transport bottles, cans, cartons, and packaged food products in hygienic production environments. It uses interconnected plastic chain plates driven by sprockets to provide stable movement, corrosion resistance, and flexible layout options for food and beverage manufacturing lines.
Compared with traditional belt conveyors, plastic chain conveyors provide a rigid conveying surface and are suitable for production lines requiring accurate positioning, smooth transfer, and continuous operation. They are commonly integrated into complete industrial conveyor systems used in food processing, beverage packaging, and automated manufacturing.
What Is a Plastic Chain Plate Conveyor and How Does It Work?
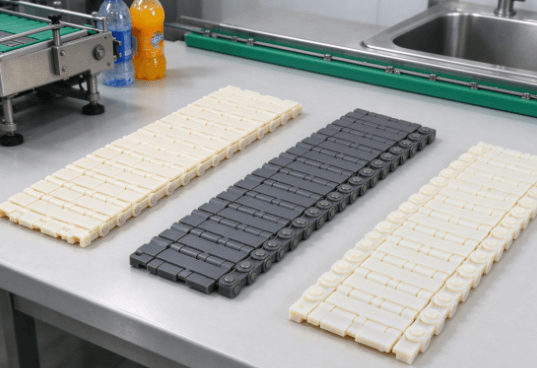
A plastic chain plate conveyor consists of modular plastic plates, sprockets, drive units, support rails, and a conveyor frame. The motor drives the sprockets, moving the connected plastic plates to create a continuous conveying surface.
Unlike conventional belt systems, modular chain conveyors can be configured with different layouts, including straight sections, curves, and accumulation areas. This makes them suitable for production environments where space utilization and product flow control are important.
Common plastic materials include:
- Polypropylene (PP): Good chemical resistance and widely used in food handling applications.
- Acetal (POM): Higher strength and lower friction for demanding conveyor applications.
- Polyethylene (PE): Good impact resistance for specific operating conditions.
Material selection depends on production requirements such as cleaning frequency, temperature range, product weight, and conveyor speed.
Manufacturers evaluating conveyor options can also compare different designs such as belt conveyor systems to understand which solution better fits their production requirements.
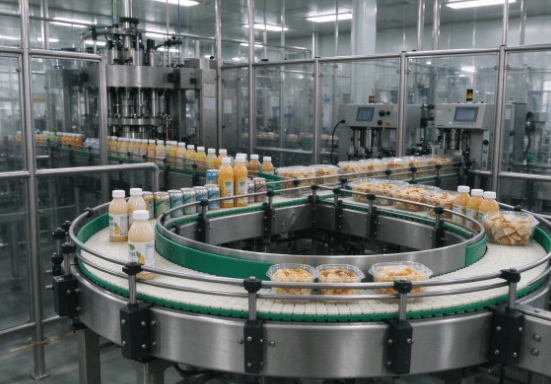
Why Are Plastic Chain Conveyors Used in Food Production?
Food and beverage manufacturers require conveying equipment that can operate reliably under moisture, cleaning processes, and continuous production conditions.
Hygienic Design and Easy Maintenance
Plastic chain conveyors are widely used in food applications because their smooth surfaces reduce material buildup and simplify cleaning procedures.
In wet production environments, corrosion resistance is especially important. Compared with traditional metal conveyor components, engineered plastic materials can provide better resistance against water and cleaning chemicals.
For production lines requiring frequent sanitation, manufacturers should consider conveyor structures designed according to food processing requirements, including suitable stainless steel conveyor solutions for areas with higher hygiene demands.
Stable Product Transportation
The rigid chain plate surface provides consistent product support during transportation.
Typical applications include:
- Beverage bottles and cans
- Food containers
- Packaging cartons
- Dairy products
- Frozen food packages
Plastic chain conveyors are often connected with filling, labeling, and packaging equipment to maintain smooth product flow.
For automated packaging operations, they can work together with conveyor automation systems to improve production line efficiency.
How to Select a Plastic Chain Conveyor for Food Applications?
Choosing a conveyor requires evaluating the entire production process rather than selecting equipment only according to conveyor size.
Important factors include:
| Selection Factor | Key Consideration |
|---|---|
| Product characteristics | Product size, weight, packaging type |
| Conveyor speed | Required production capacity |
| Cleaning requirements | Water, chemicals, sanitation frequency |
| Temperature conditions | Operating environment and material performance |
| Layout design | Curves, transfers, and production space |
For example, beverage factories usually focus on smooth bottle handling and continuous operation, while food packaging facilities may require more flexible layouts and accumulation functions.
A proper conveyor design should also consider future expansion, maintenance accessibility, and integration with other equipment.
Plastic Chain Conveyor Applications in Food and Beverage Industries
Beverage Bottling and Packaging Lines
Plastic chain conveyors are widely used in beverage manufacturing for transporting:
- Bottles
- Cans
- Cartons
- Shrink-wrapped packages
They help connect different production stages, including filling, labeling, inspection, and packaging.
For factories requiring customized transportation layouts, custom conveyor systems can be designed according to production space, product flow, and automation requirements.
Food Processing and Packaging
In food production facilities, plastic chain conveyors are suitable for transporting packaged products such as:
- Ready-to-eat meals
- Dairy products
- Frozen food
- Bakery products
The conveyor configuration should match product handling requirements, especially where product orientation and transfer accuracy are important.
Plastic Chain Conveyor vs Other Conveyor Types
| Conveyor Type | Advantages | Common Applications |
|---|---|---|
| Plastic chain conveyor | Flexible design, hygienic operation, corrosion resistance | Food and beverage production |
| Belt conveyor | Simple structure and economical operation | General material handling |
| Roller conveyor | Suitable for rigid products and pallets | Logistics and warehouse systems |
Different conveyor types serve different purposes. For example, belt conveyors may be preferred for simple transportation, while plastic chain systems are often selected for production lines requiring curves, accumulation, or frequent cleaning.
You can also learn more about different types of conveyor systems before selecting equipment for a specific application.
Choosing the Right Plastic Chain Conveyor Manufacturer
Selecting a suitable conveyor solution requires understanding not only the equipment design but also the manufacturer’s engineering capability.
Important evaluation points include:
- Experience with similar production environments
- Ability to customize conveyor layouts
- Understanding of food industry requirements
- Support for system integration
A qualified conveyor supplier should be able to provide technical recommendations based on product characteristics, production speed, and factory layout.
Leyu Conveyor provides industrial conveying solutions for different manufacturing applications, including food processing, packaging, and automated production lines.
FAQ
Are plastic chain conveyors suitable for food and beverage production?
Yes. Plastic chain conveyors are widely used in food and beverage industries because they provide stable transportation, corrosion resistance, and flexible cleaning options.
What products can plastic chain plate conveyors transport?
They can transport bottles, cans, cartons, trays, and packaged food products. The conveyor design depends on product weight, size, and production requirements.
What is the difference between a plastic chain conveyor and a belt conveyor?
Plastic chain conveyors use modular plastic plates connected together, while belt conveyors use a continuous flexible belt. Plastic chain systems usually provide better flexibility for curved layouts and accumulation applications.
How do I choose the right conveyor system for food production?
Selection should consider product type, production speed, cleaning requirements, temperature conditions, and integration with existing automation equipment.
Reference Sources
- ISO 22000 Food Safety Management Systems
https://www.iso.org/iso-22000-food-safety-management.html - FDA Food Contact Materials
https://www.fda.gov/food/packaging-food-contact-substances-fcs - Conveyor Equipment Manufacturers Association (CEMA)
https://cemanet.org/